Comparative Technical Analysis of Raw Material Selection in Industrial Plastic Pail Production: PP-H, PP-C, and HDPE
Selecting the correct raw material in industrial packaging and plastic pail production is a critical engineering decision that directly determines the mechanical strength, chemical resistance, temperature performance, and shelf-life of the product. Commonly used in injection molding processes, Homopolymer Polypropylene (PP-H), Copolymer Polypropylene (PP-C), and High-Density Polyethylene (HDPE) exhibit distinct differences in terms of flexibility, impact resistance, barrier properties, and thermal endurance.
1. Comprehensive Raw Material Comparison Matrix
The following matrix summarizes the technical performance of the three core raw material groups according to industrial criteria:
| Comparison Criterion |
Homopolymer (PP-H) |
Copolymer (PP-C) |
Polyethylene (HDPE) |
| Flexibility & Impact Resistance |
Low flexibility (Rigid). Good at room temperature, brittle under hard impacts. |
Good flexibility. High impact resistance against drops and collisions. |
Very high flexibility. Absorbs impacts elastically, unbreakable. |
| Cold Environment Performance |
Poor. Becomes brittle at and below; high risk of cracking. |
Very good. Retains flexibility and strength down to . |
Excellent. Safely used in freezer environments down to . |
| Hot Filling Suitability |
Very good. Suitable for hot fillings between and . |
Good. Maintains its form up to approximately . |
Low. Withstands a maximum of ; softens above this threshold. |
| Chemical Resistance |
Good. Resistant to acids, bases, and water-based products. |
Good. Resistant to standard industrial chemicals. |
Very high. Most suitable for heavy acids, solvents, and hazardous materials. |
| Aroma Permeability |
Medium-Good. Offers the best barrier among the three due to its high crystalline structure. |
Medium. Slightly more permeable than homopolymer due to its flexible molecular structure. |
Poor-Medium. Higher transmission rate for oxygen and volatile aromas. |
| Stacking / Crush Resistance |
Very high. Does not crush during vertical stacking thanks to its rigid body. |
Medium-Good. Minor wall deflection may occur during high pallet stacking. |
Medium. Flexes under heavy top stacking loads due to its flexible body structure. |
| Print & IML Compatibility |
Excellent. Glossy and smooth surface is ideal for IML and offset printing. |
Very good. Fully compatible with IML and offset printing despite a slightly matte surface. |
Limited. Due to low surface tension, labeling or partial IML is applied. |
| Primary Sectors |
Construction (paint, plaster), hot-fill foods, dry foods. |
Frozen foods, ice cream, dairy products, construction chemicals. |
Heavy chemicals, lubricants, agrochemicals, deep-freeze foods. |
2. Polypropylene (PP) Classification and Technical Properties
Polypropylene is generally evaluated in three main structures: Homopolymer PP, Block/Impact Copolymer PP, and Random Copolymer PP.
2.1. Homopolymer Polypropylene (PP-H)
Obtained through the polymerization of a single monomer type (propylene), this polymer features high rigidity and chemical resistance. It is designed for applications requiring high load-bearing capacity under constant temperature conditions.
- High Rigidity and Strength: Thanks to its uniform molecular chain structure, it is significantly more rigid compared to copolymers. This property provides superior resistance to crushing when pails are stacked on top of each other.
- Thermal and Chemical Resistance: Offers exceptional protection against acids, bases, and organic solvents. Its high melting point enables hot-filling processes at .
- Low Temperature Limit: Tends to become brittle at temperatures below ; impact resistance drops in cold storage conditions.
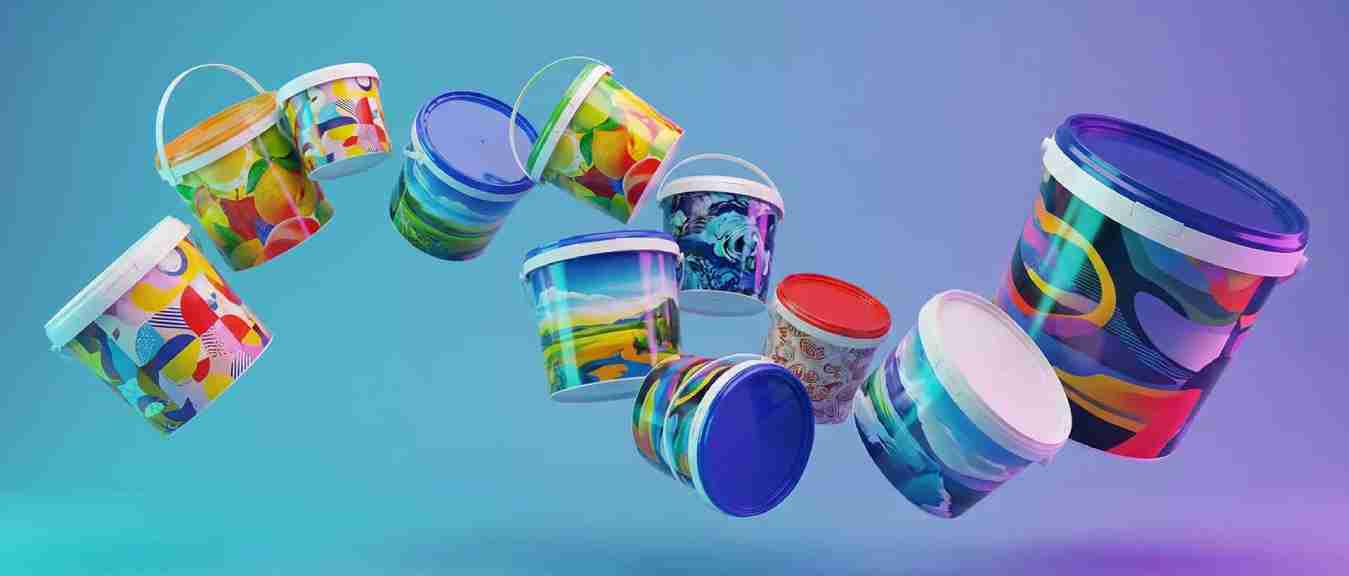
- Surface Quality and Printability: Smooth and glossy surface quality creates an impeccable foundation for In-Mold Labeling (IML) and offset printing applications.
Aroma Permeability and Barrier Solutions in Homopolymer
Although PP-H possesses a medium-good aroma barrier compared to most polymers, it is not completely impermeable. Due to its non-polar structure, while it resists water-based aromas, oil-based aromas and volatile organic compounds (VOCs) can diffuse through the polymer chains over time. The following engineering solutions are applied for sensitive products requiring high aroma retention:
- EVOH Barrier Layer: An Ethylene Vinyl Alcohol layer integrated via IML technology minimizes gas and aroma transmission.
- Inner Bag (Liner) Utilization: Aluminum foil-laminated or high-barrier polyamide (PA/PE) inner bags completely trap aromas.
2.2. Copolymer Polypropylene (PP-C)
Produced by incorporating controlled ratios of ethylene into the propylene monomer. It offers higher impact and lower temperature resistance compared to homopolymers.
- High Impact Resistance: Ethylene segments impart flexibility to the plastic, increasing resistance to drops, impacts, and shocks.
- Cold Chain Compatibility: Retains its flexibility down to , offering safe usage in cold storage facilities and frozen food logistics.
- Classification:
- Block Copolymer (PP-B): Provides maximum impact and cold resistance with a higher ethylene content; most widely used in heavy-duty industrial pails.
- Random Copolymer (PP-R): Utilized in specialized food packaging where transparency and thermal resistance are required.
3. High-Density Polyethylene (HDPE)
Produced via the polymerization of ethylene monomer, HDPE stands out with its exceptional flexibility, impact-damping capability, and superior chemical resistance.
- Superior Drop and Impact Resistance: Features a much more flexible structure than PP types; does not crack during high-altitude drops and absorbs impacts via elastic deformation.
- Extreme Cold Performance: Maintains its mechanical integrity even in freezer conditions down to .
- Chemical Compatibility: Demonstrates superior resistance to strong acids, bases, corrosive chemicals, and solvents compared to polypropylene. Consequently, the vast majority of UN-certified industrial pails and drums required for hazardous material transport are manufactured from HDPE.
- Limitations: Features a lower hot-filling limit of approximately ; softening begins above this threshold. Due to low surface tension, traditional IML applications require specialized surface treatment (corona, etc.).
4. Summary Engineering Selection Guide
- Homopolymer (PP-H) should be chosen if high stacking performance, hot filling, and superior visual IML quality are priorities.
- Copolymer (PP-C) is the most rational solution when a balance of cold chain logistics, impact risk, and aesthetic packaging is required.
- Polyethylene (HDPE) should be selected in the presence of heavy chemicals, UN-certified hazardous material transport, or deep-freeze (below ) conditions.